2-25 Hydraulic Block Press
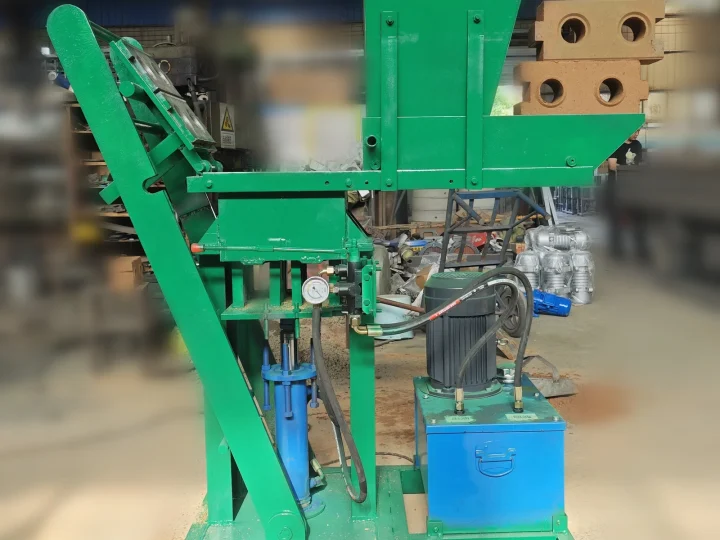
The 2-25 photographs show a hopper, pressing frame and separate hydraulic power unit. The operator handles feeding and removal; this is not a fully automated block production line.
View product →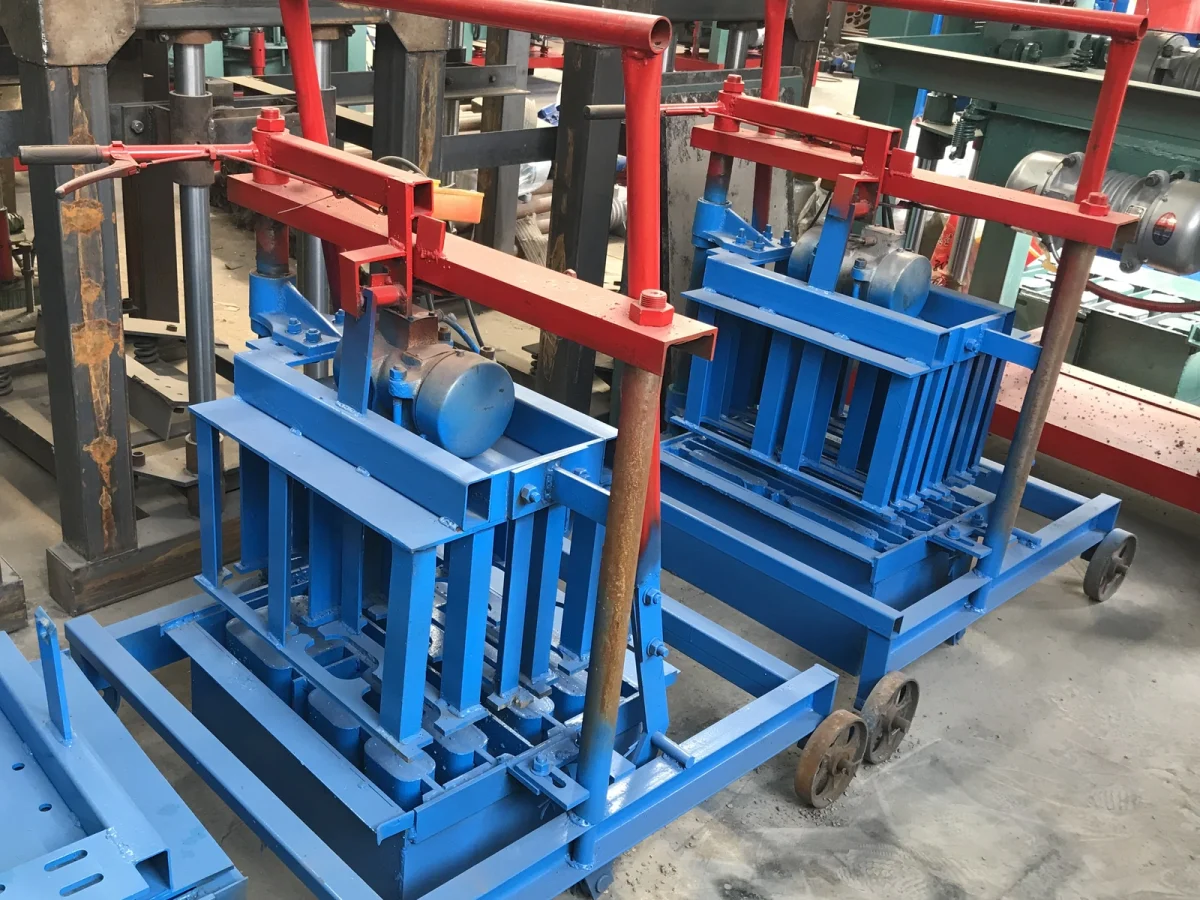
Original photographs and labelled component panels. Installed machines, colours and workshop stock illustrate configurations; the quotation defines what is supplied.
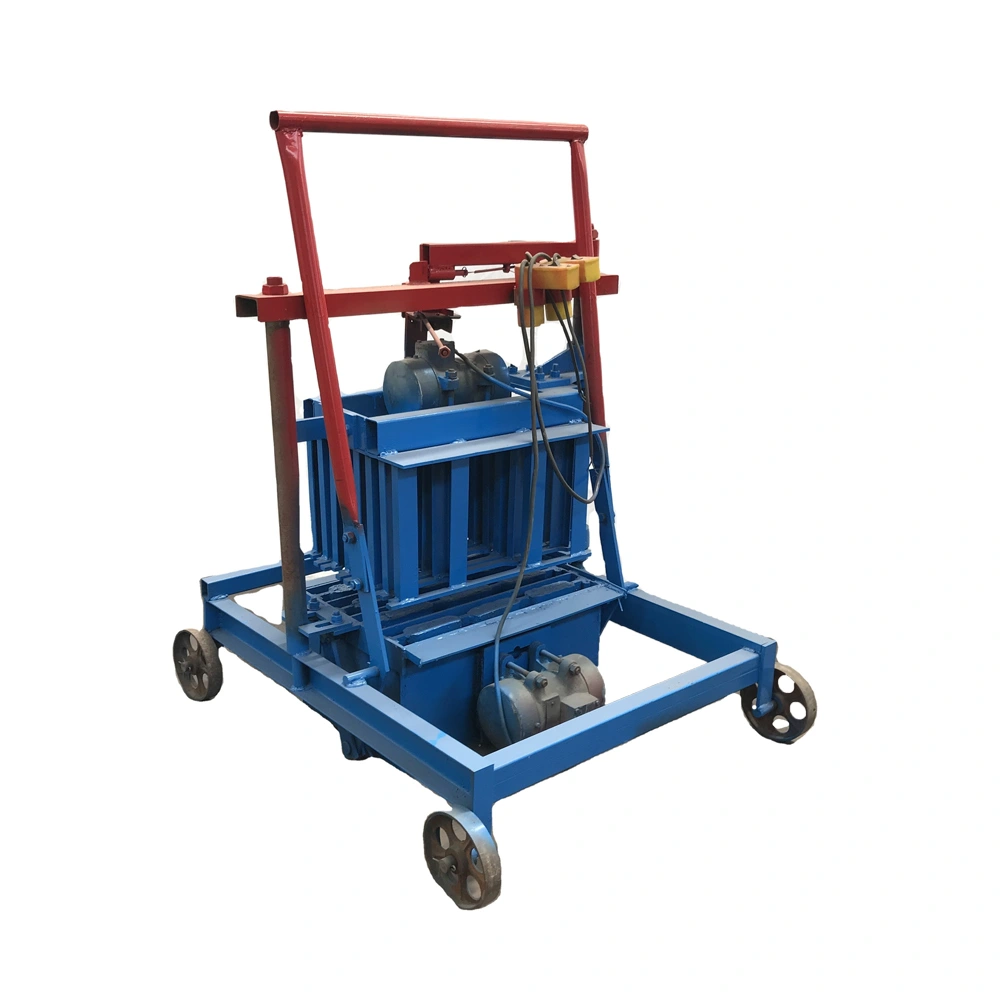
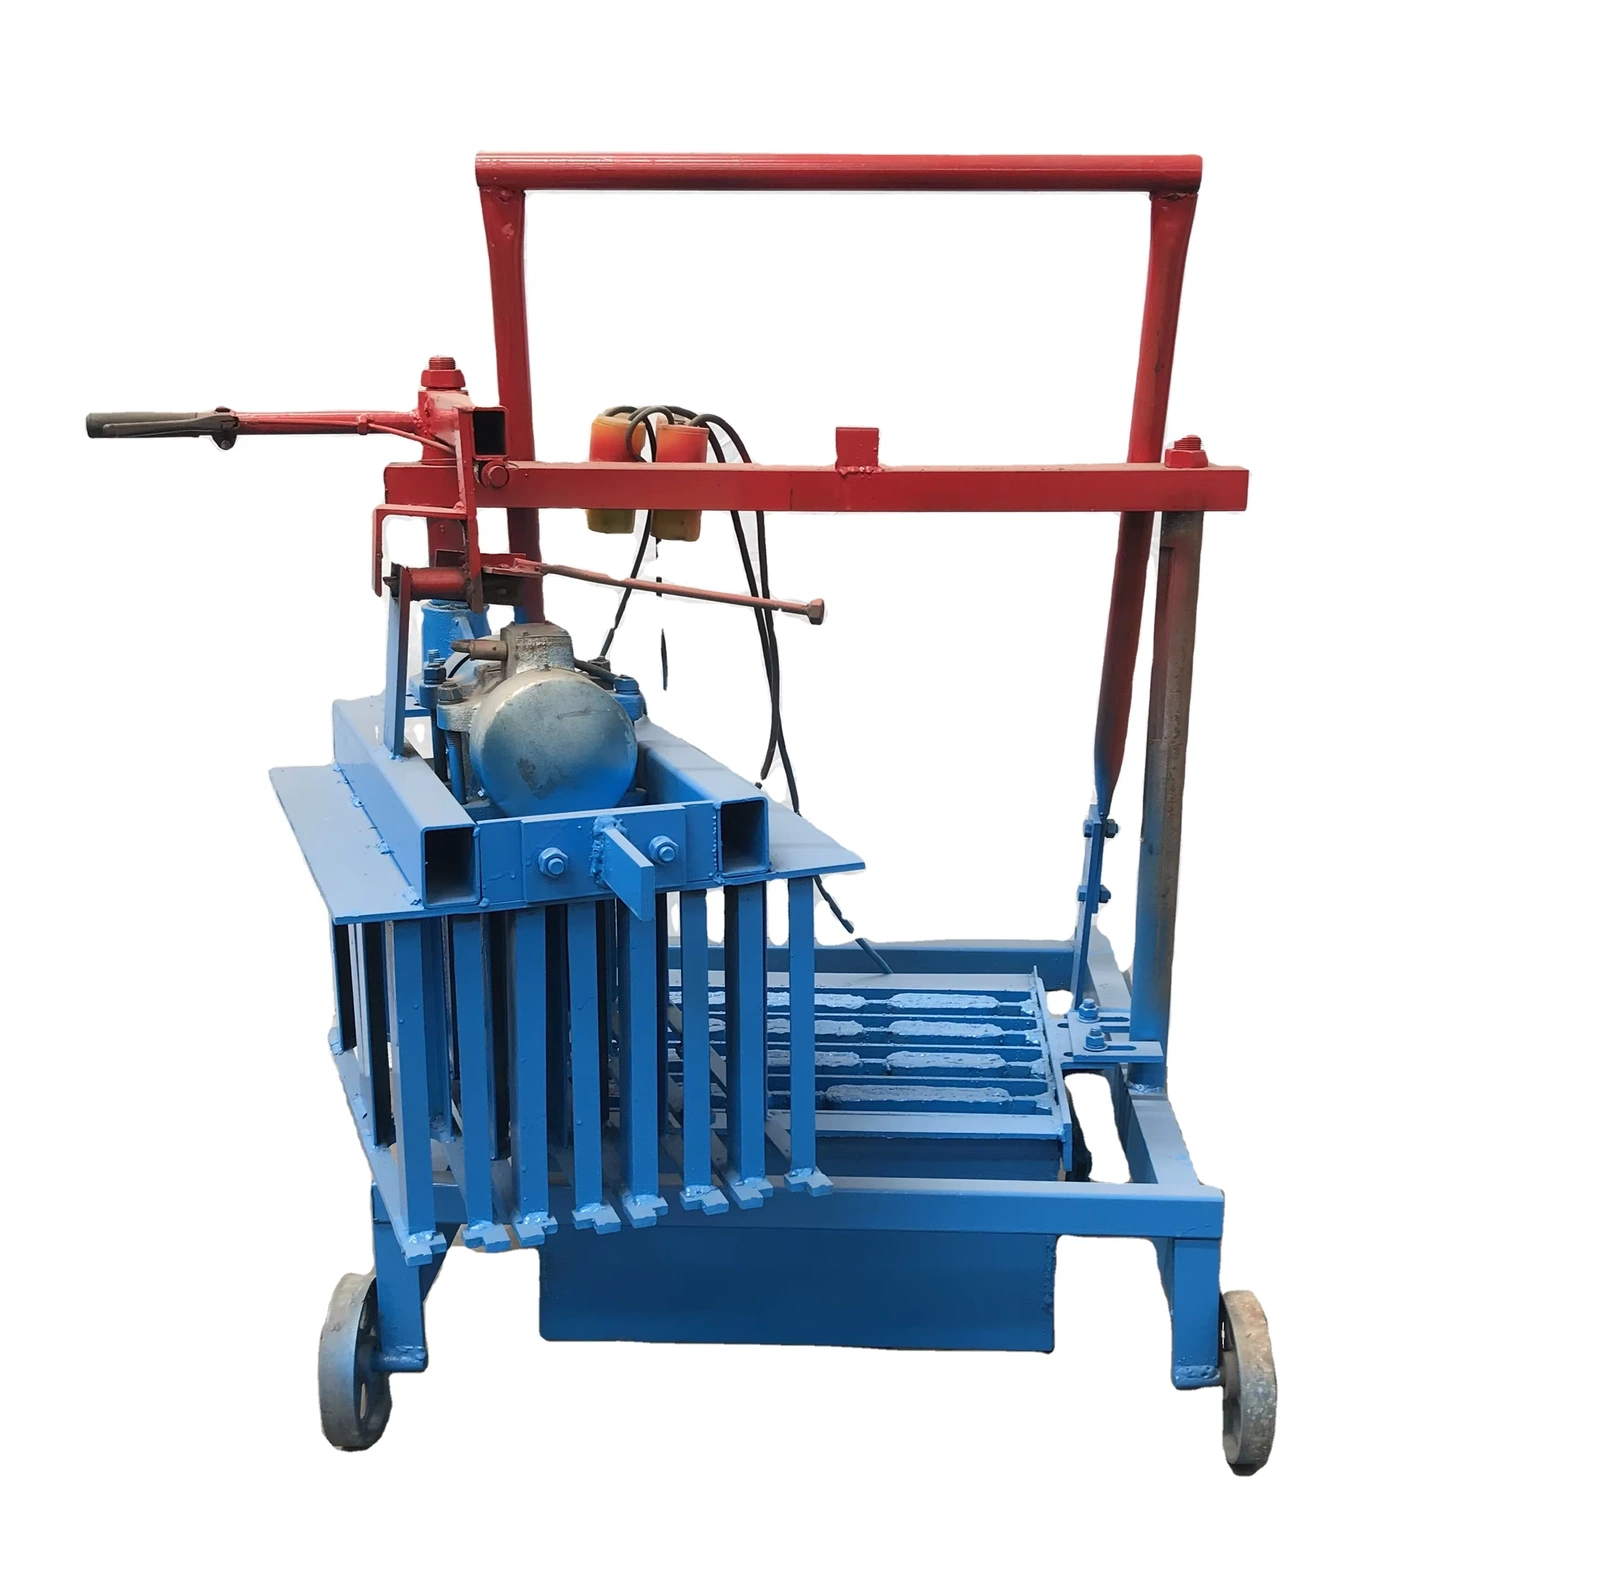
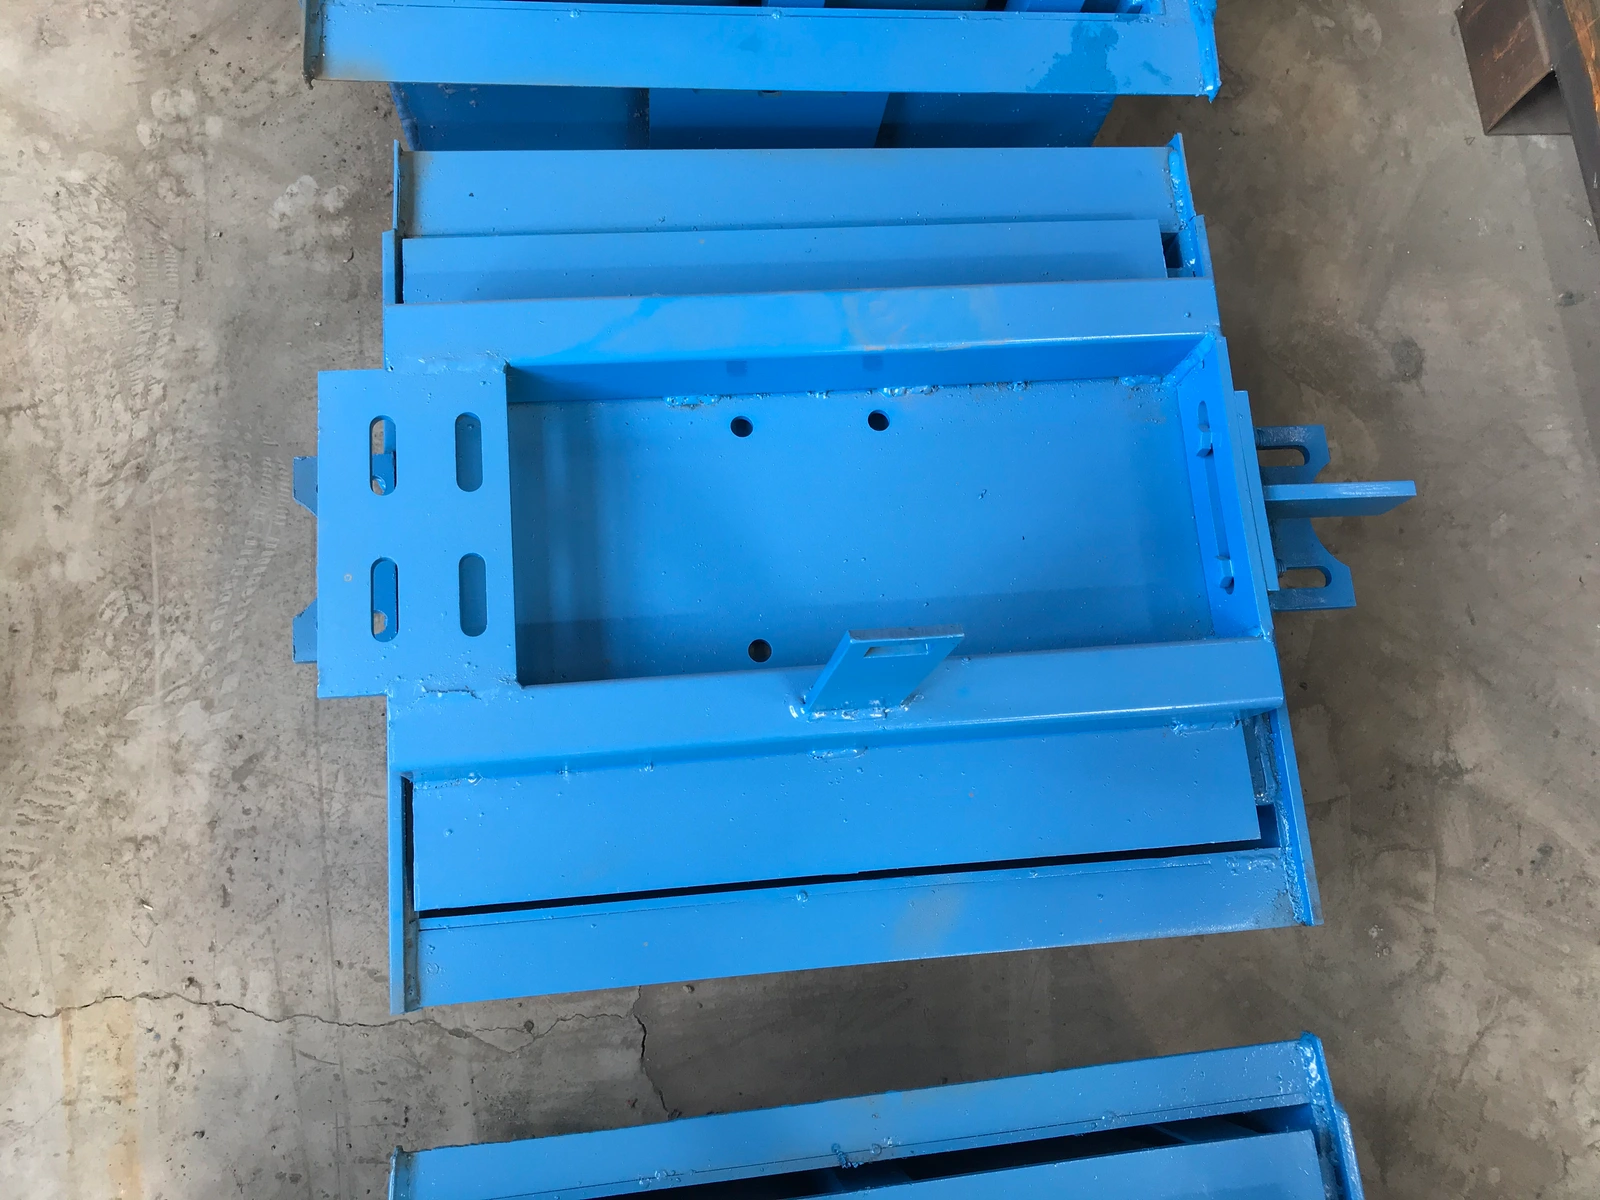
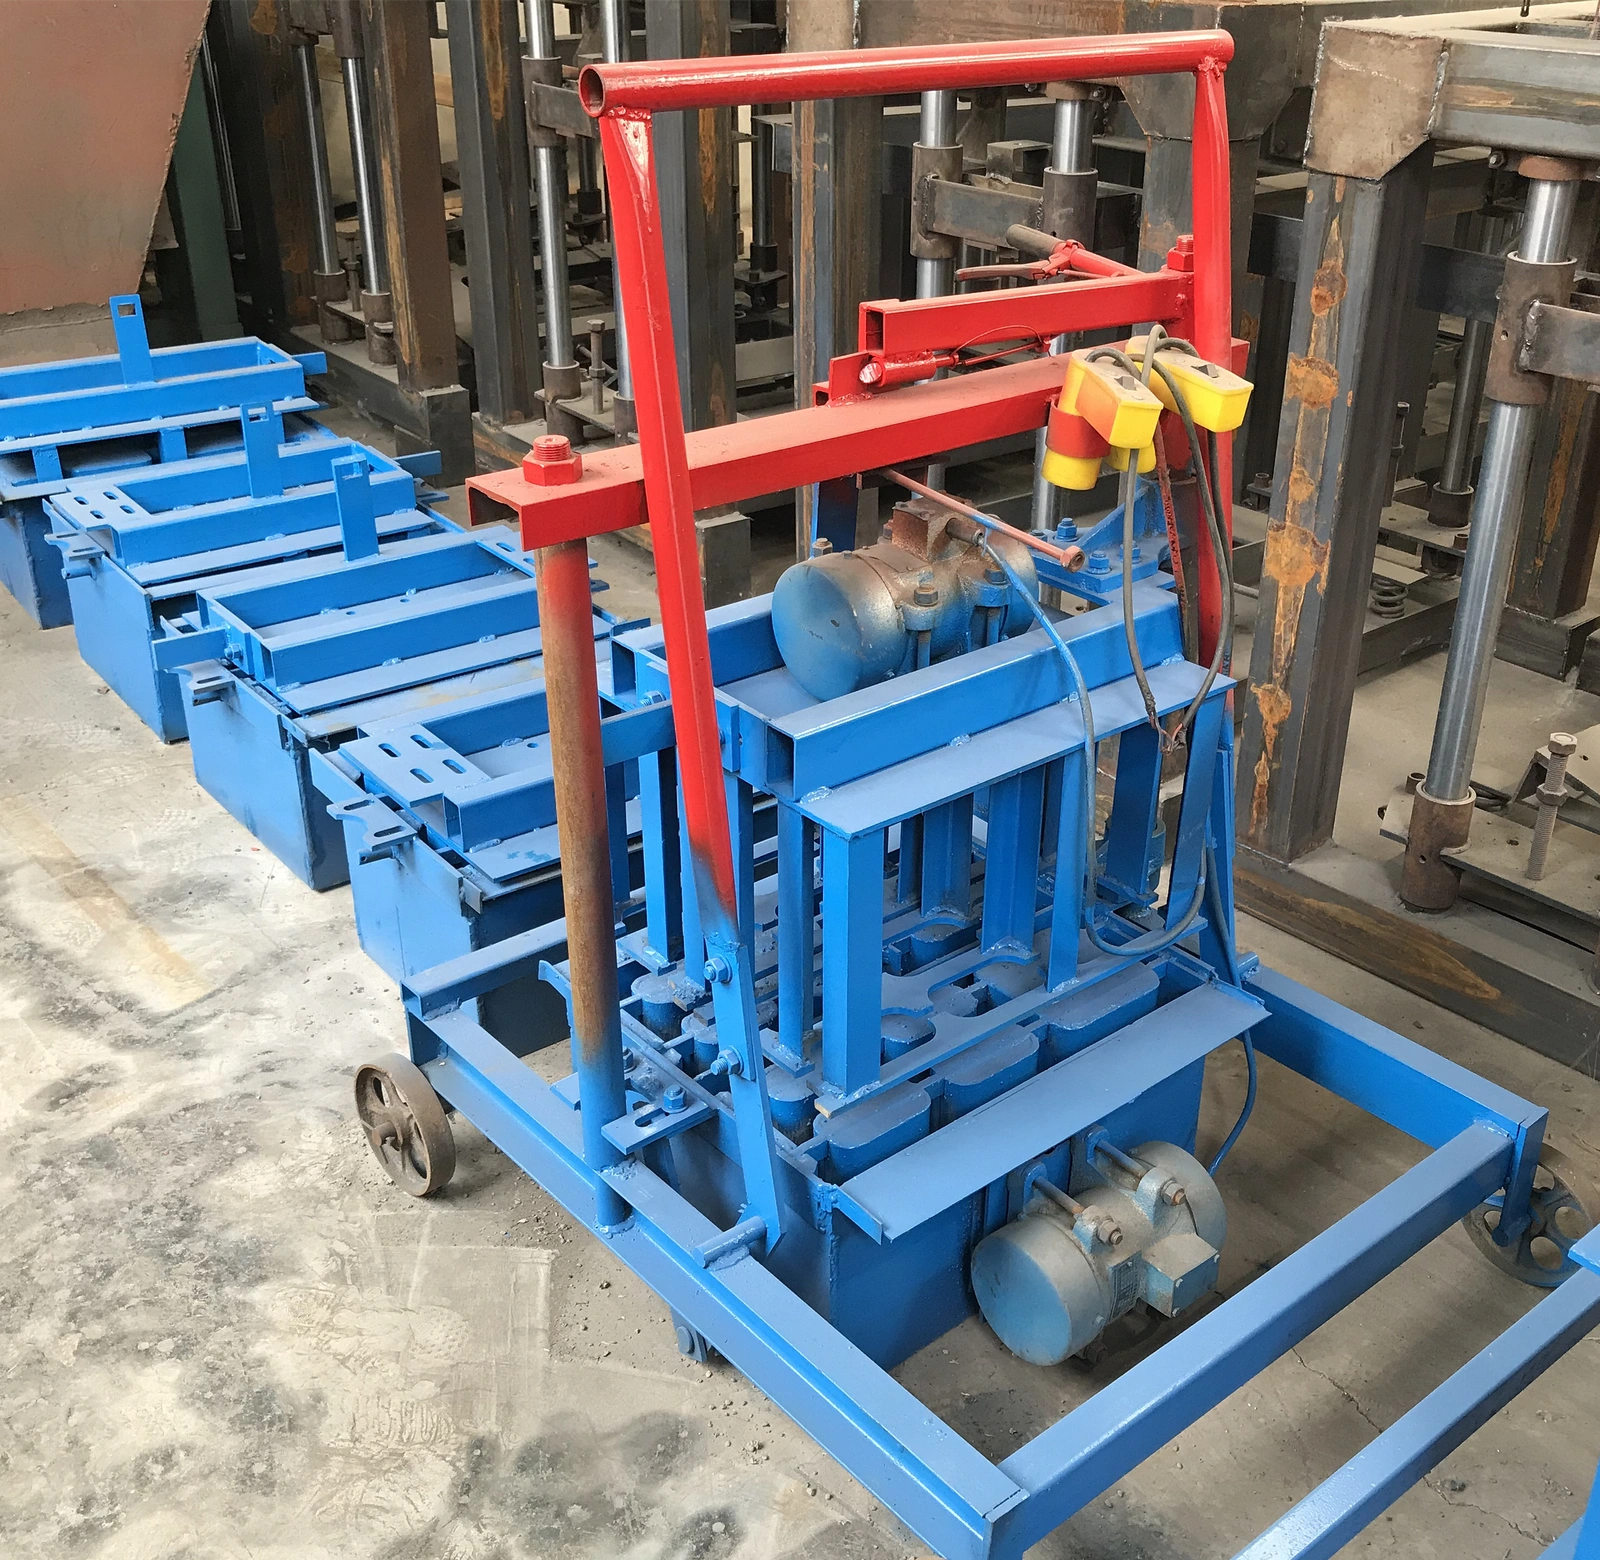
2-45A Manual-Control Block Making Machine
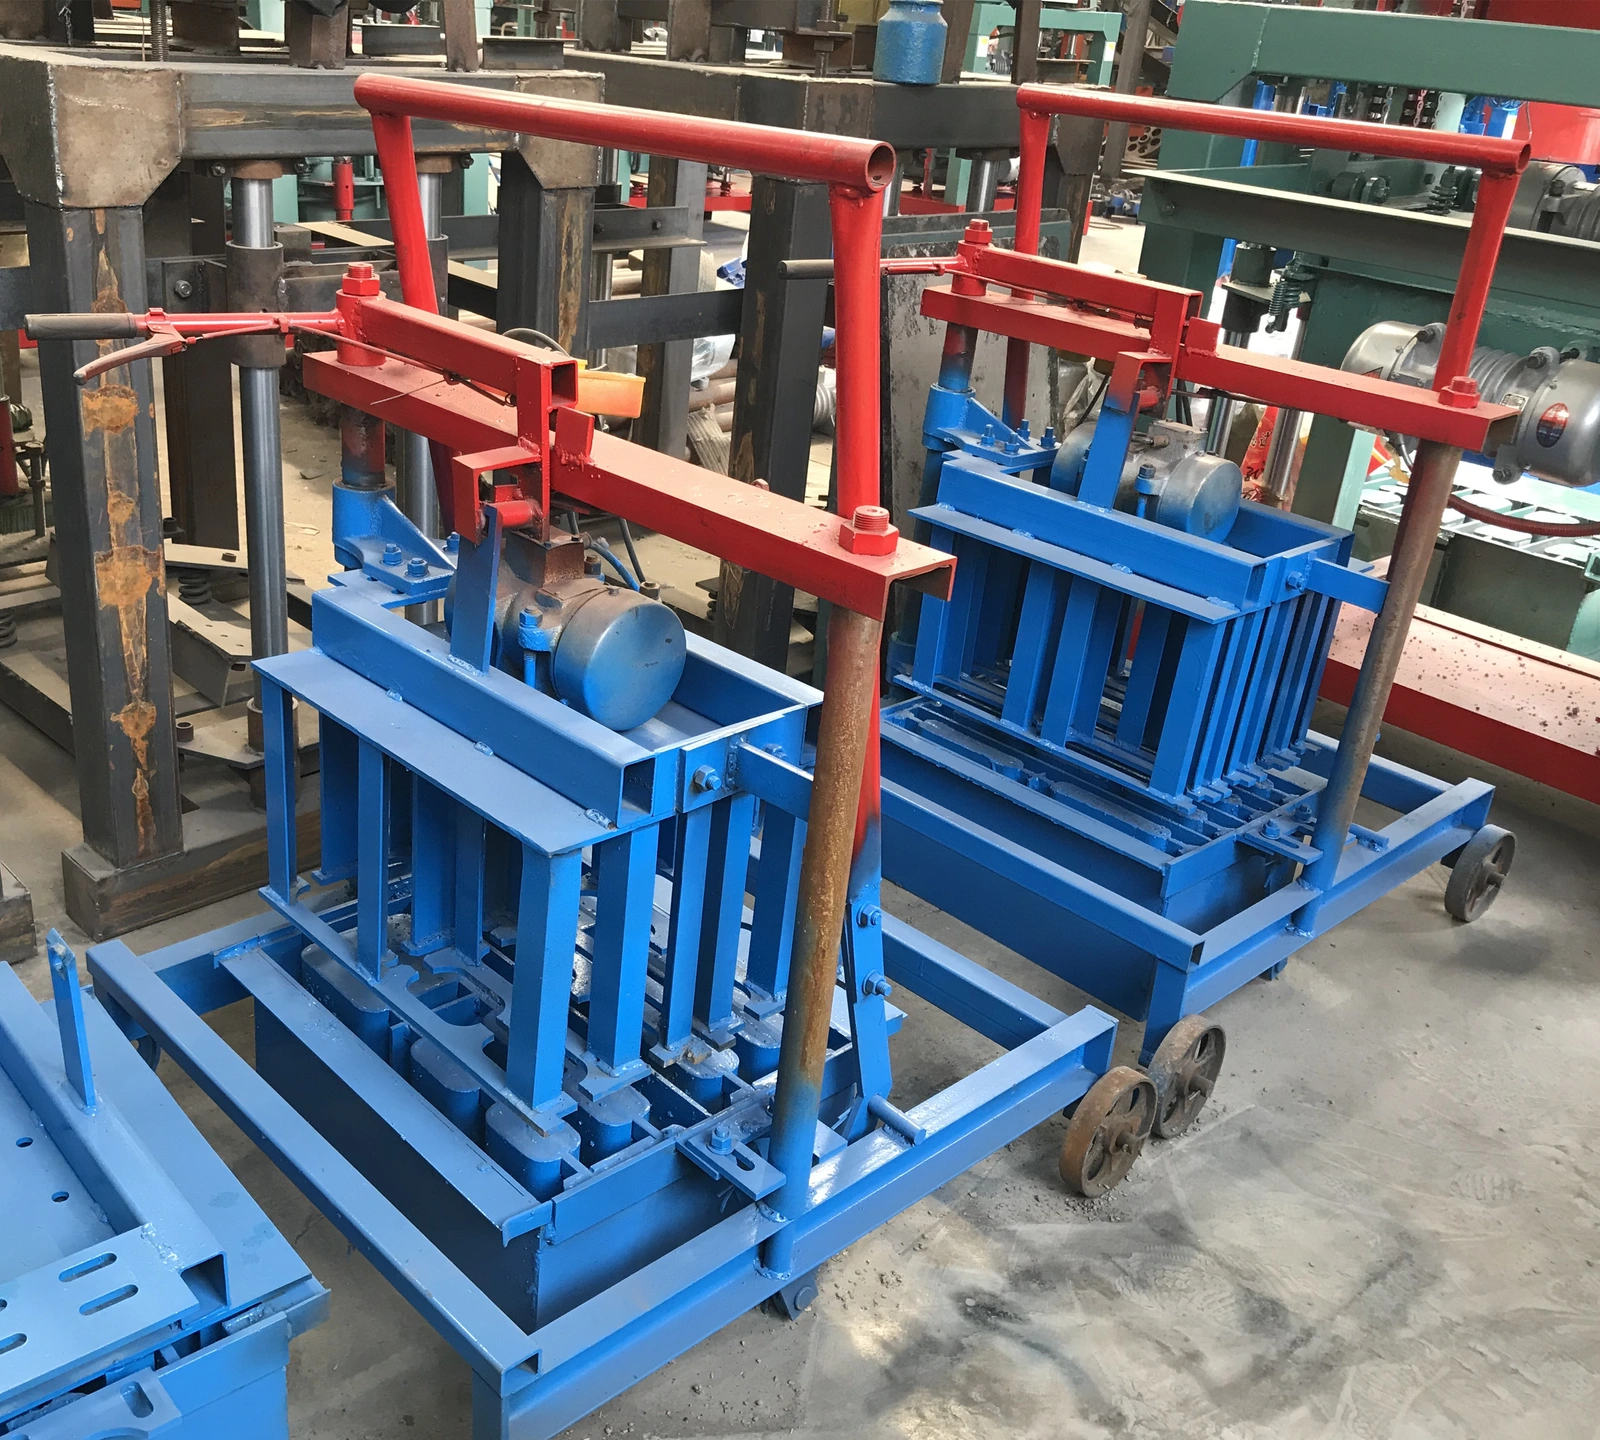
The 2-45A combines a wheeled mould frame, manual operating levers and a motor-driven vibration assembly. It forms blocks against a suitable prepared surface; mould selection defines the block pattern and dimensions.
| Voltage options; exact motor to confirm | 110V-440V |
|---|---|
| Source mould/block size options | 240*115*53mm, 390*190*190mm, 240*190*190mm, 390*150*190mm, 390*120*190mm, 390*100*190mm |
| Listed mass | 170 kg |
| Source moulding cycle; full workflow separate | 45s |
| Source staffing range | 1-2 Worker |
| Selected power option | 1.1KW |
| Parameters to confirm | Confirm missing parameters and delivery contents for the exact configuration. |
The 2-45A combines a wheeled mould frame, manual operating levers and a motor-driven vibration assembly. It forms blocks against a suitable prepared surface; mould selection defines the block pattern and dimensions.
The source dimension field contains a voltage range and is unusable as a machine size. Daily output figures lack a matched mould and working-cycle basis, so they are not adopted as guaranteed capacity. Confirm the motor plate, mould cavities and handling sequence.
Match the mould and mix to the required block. Plan a level working area, material feeding, removal of fresh blocks and curing space. A vibration cycle alone is not the complete time for mixing, feeding and handling.
Ask for the model plate, operating manual and itemised delivery list. Record tooling, wear parts and packing separately so that the delivered equipment can be checked against the order.
Confirm missing parameters and delivery contents for the exact configuration.
The 2-45A combines a wheeled mould frame, manual operating levers and a motor-driven vibration assembly. It forms blocks against a suitable prepared surface; mould selection defines the block pattern and dimensions.
Confirm supplied accessories, packing weight and dimensions, transit protection and delivery terms.
Confirm missing parameters and delivery contents for the exact configuration.
Not necessarily. Request a mould drawing and cavity arrangement for the selected block.
No. The source shows manual operating levers with a motor-driven vibration assembly.
No. Feeding, mould cavities, handling, mix and curing arrangements determine actual production.
Provide the block drawing, desired output and mix materials. Agree moulds, electrical version and workflow before ordering.
The source dimension field contains a voltage range and is unusable as a machine size. Daily output figures lack a matched mould and working-cycle basis, so they are not adopted as guaranteed capacity. Confirm the motor plate, mould cavities and handling sequence.
State the model or part, measurements and quantity. Ask for equipment, accessories and documents to be itemised separately.
The 2-25 photographs show a hopper, pressing frame and separate hydraulic power unit. The operator handles feeding and removal; this is not a fully automated block production line.
View product →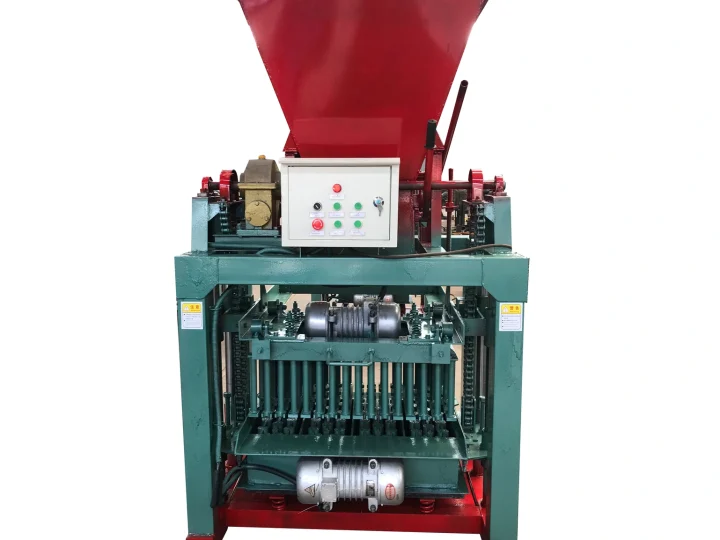
The 4-35C has a feed hopper above the mould and a framed vibration assembly. It forms concrete blocks using a selected mould; the finished-block photographs show why the mould choice is part of the order.
View product →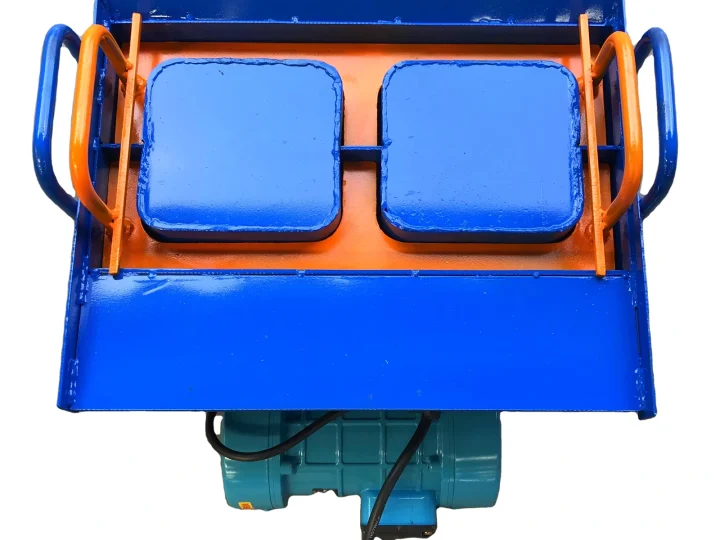
The photographs show a portable mould box with a motor below it and removable upper pieces. It makes sense as a compact block-forming tool, not the large automated brick machine implied by the old title.
View product →