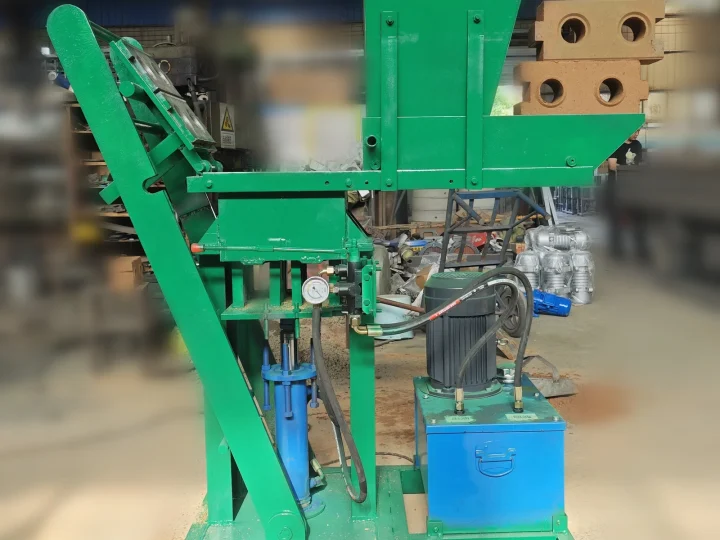
2-25 Hydraulic Block Press
The 2-25 photographs show a hopper, pressing frame and separate hydraulic power unit. The operator handles feeding and removal; this is not a fully automated block production line.
View product →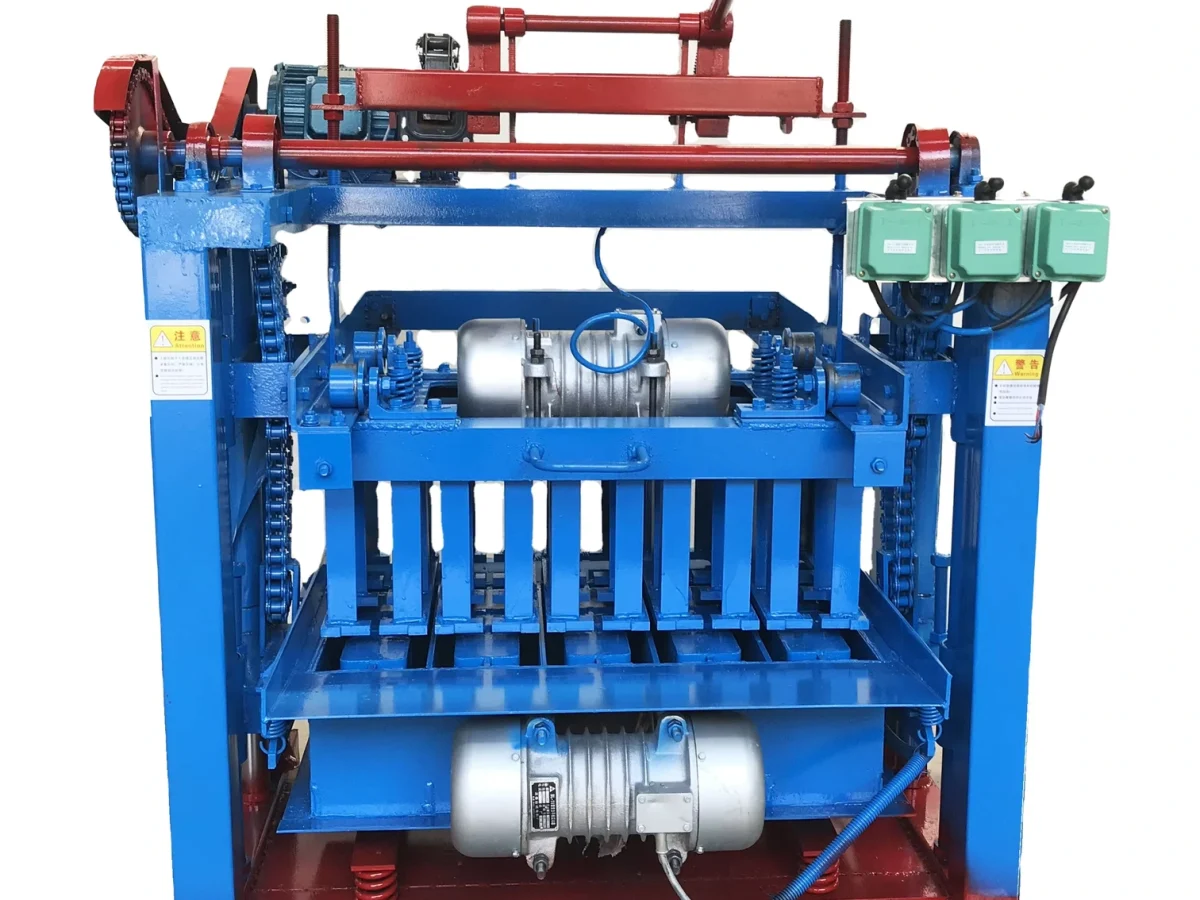
Original photographs and labelled component panels. Installed machines, colours and workshop stock illustrate configurations; the quotation defines what is supplied.
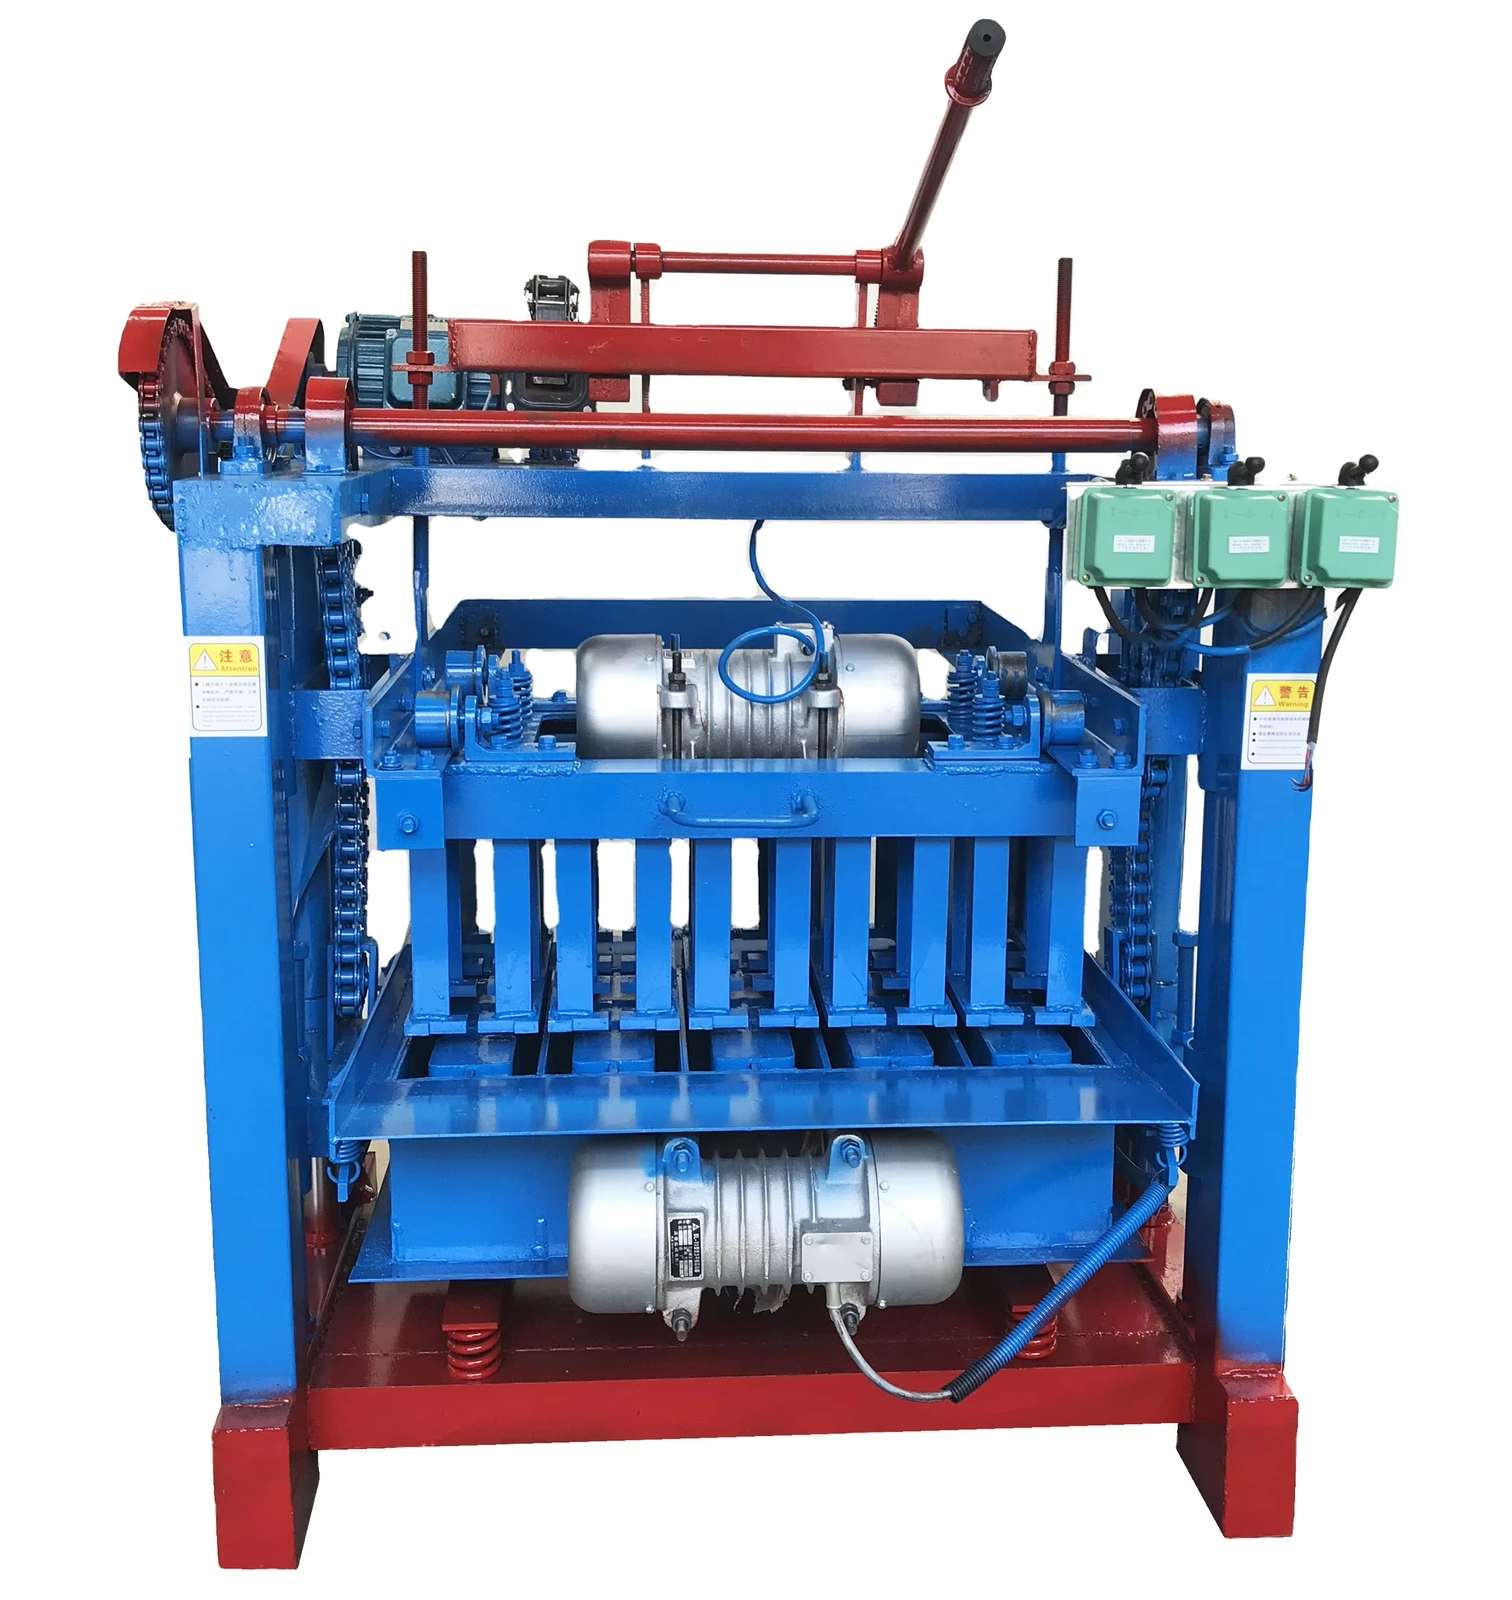
4-35A Mobile Concrete Block Machine
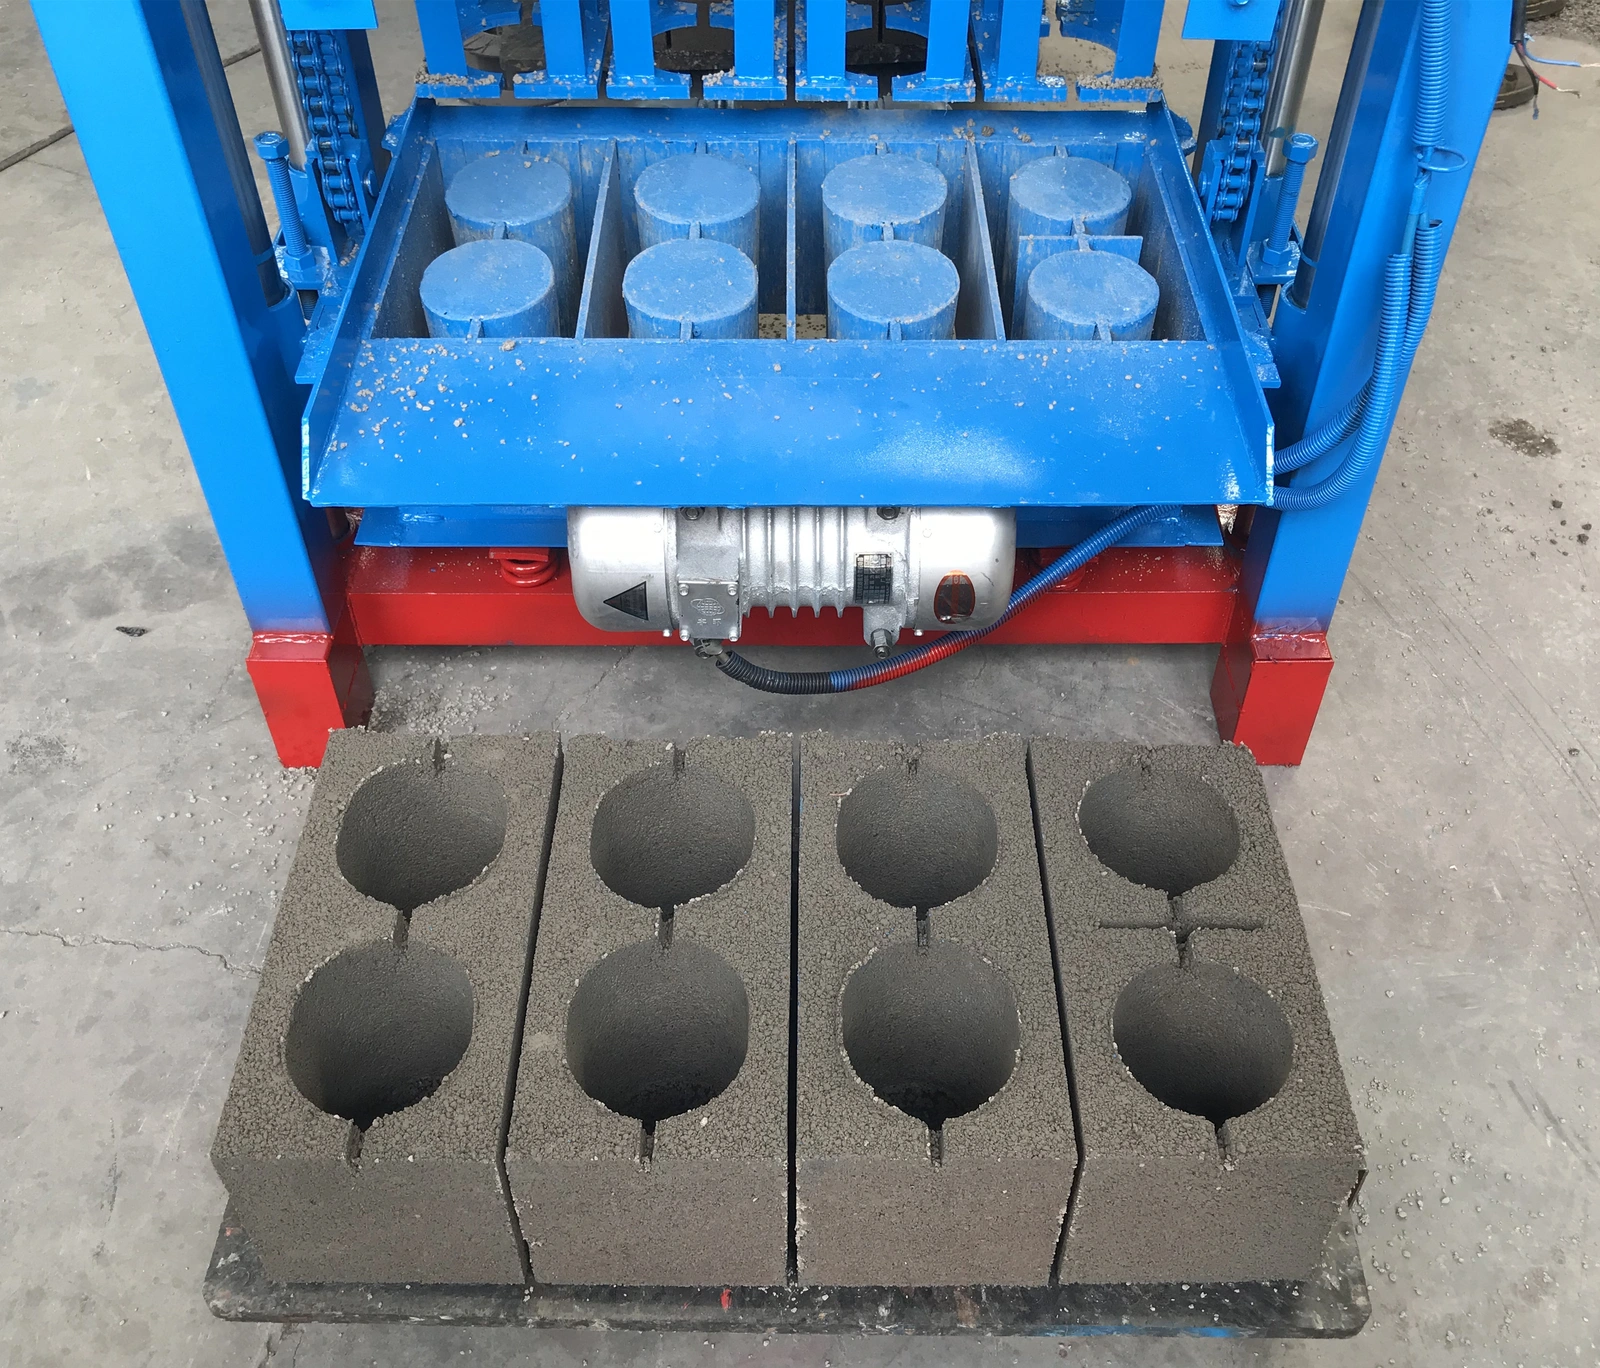
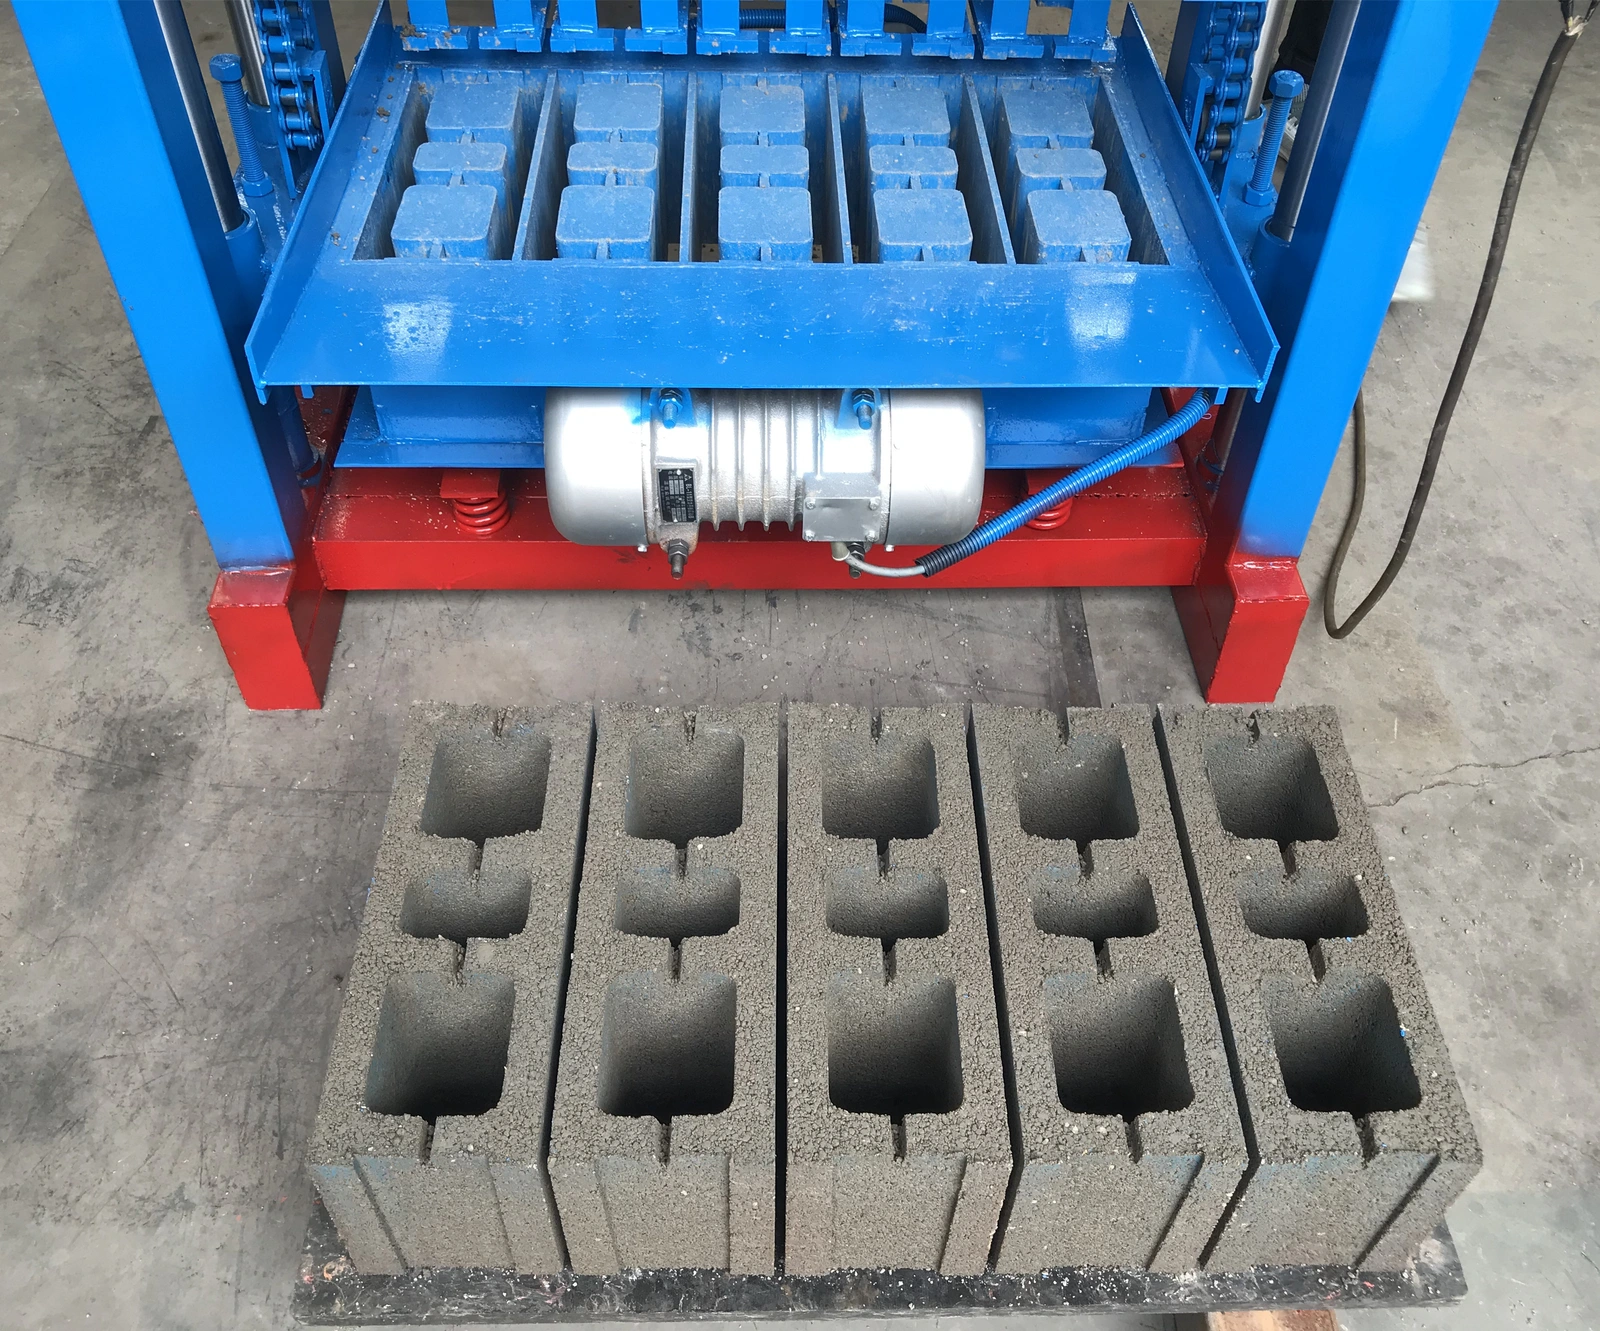
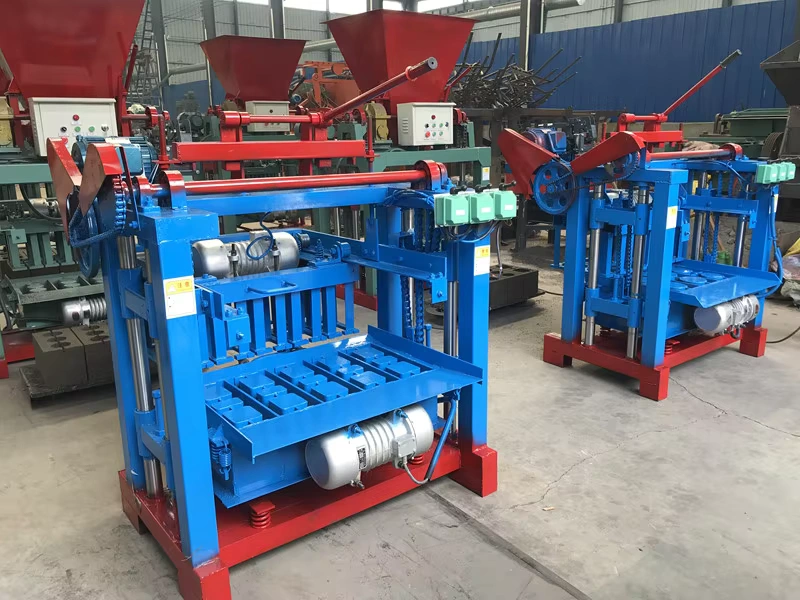
The 4-35A has a framed mould assembly with vibration motors and operating levers. The source pictures show different hollow-block moulds and output examples on the working surface.
| Supply options | 220V/380V or customized |
|---|---|
| Listed dimensions; scope to confirm | 1340*1280*1610mm |
| Block-size examples; mould-dependent | 400*100*200 mm, 400*120*200 mm, 200*100*60 mm, 300*150*100 mm, 400*150*200 mm, 240*115*90 mm, 200*200*60 mm, 150*150*100 mm, 400*200*200 mm, 230*220*115 mm |
| Listed weight | 640 kg |
| Listed forming cycle | 35s |
| Listed operator requirement | 2-3Worker |
| Selected power option | 5.5KW |
| Parameters to confirm | Confirm missing parameters and delivery contents for the exact configuration. |
The 4-35A has a framed mould assembly with vibration motors and operating levers. The source pictures show different hollow-block moulds and output examples on the working surface.
An automatic source label does not identify which steps are powered. Confirm material feeding, mould lifting, machine travel and block removal separately. The quoted mould and control layout determine the practical workflow.
Send the finished-block drawing, cavity layout and proposed mix. Confirm whether blocks are formed on the ground or on pallets and how they are moved to curing. Mixing, handling and curing equipment should be listed separately from the forming machine.
Request an output assessment tied to the selected mould and actual operating cycle. Include feeding, demoulding, changeovers and handling rather than comparing an unexplained shift maximum. Specify moulds, controls and ancillary equipment in the quote.
Confirm missing parameters and delivery contents for the exact configuration.
The 4-35A has a framed mould assembly with vibration motors and operating levers. The source pictures show different hollow-block moulds and output examples on the working surface.
Confirm supplied accessories, packing weight and dimensions, transit protection and delivery terms.
Confirm missing parameters and delivery contents for the exact configuration.
Start with the finished-block drawing and match its cavities and machine interfaces.
A source capacity field needs a defined mould, mix, operating cycle and handling workflow before it can be compared.
Only if listed separately in the quotation. The forming machine does not replace these operations.
No. Ask for material trials and the testing applicable to the proposed block and use.
An automatic source label does not identify which steps are powered. Confirm material feeding, mould lifting, machine travel and block removal separately. The quoted mould and control layout determine the practical workflow.
State the model or part, measurements and quantity. Ask for equipment, accessories and documents to be itemised separately.
The 2-25 photographs show a hopper, pressing frame and separate hydraulic power unit. The operator handles feeding and removal; this is not a fully automated block production line.
View product →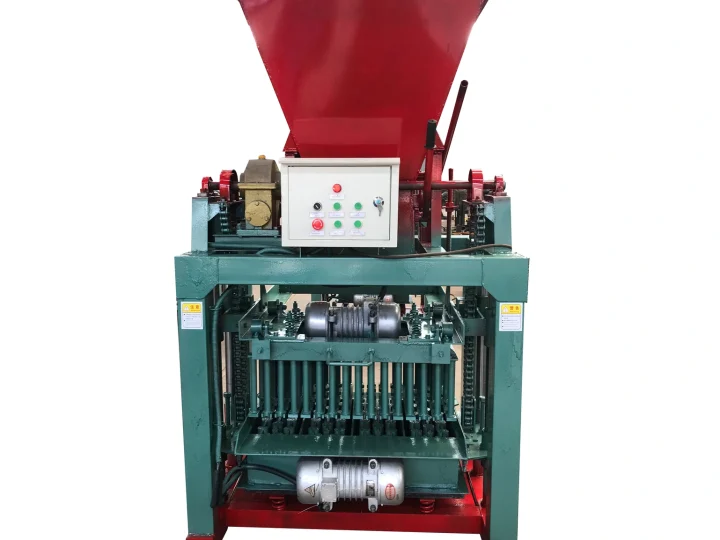
The 4-35C has a feed hopper above the mould and a framed vibration assembly. It forms concrete blocks using a selected mould; the finished-block photographs show why the mould choice is part of the order.
View product →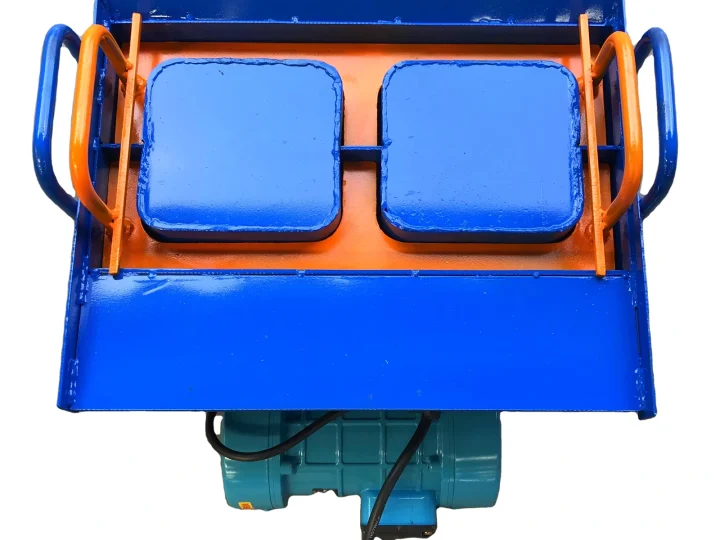
The photographs show a portable mould box with a motor below it and removable upper pieces. It makes sense as a compact block-forming tool, not the large automated brick machine implied by the old title.
View product →